LuxMV
See What Matters.
Discuss a project
Electronics & AOI Inspection

PCB Solder Joint Inspection Lighting

To separate solder bridging, insufficient wetting, and component polarity, use a multi-tier RGB ring light. High-angle red, mid-angle green, and low-angle blue turn the fillet slope into separate colors. Send the board to match the ring series.

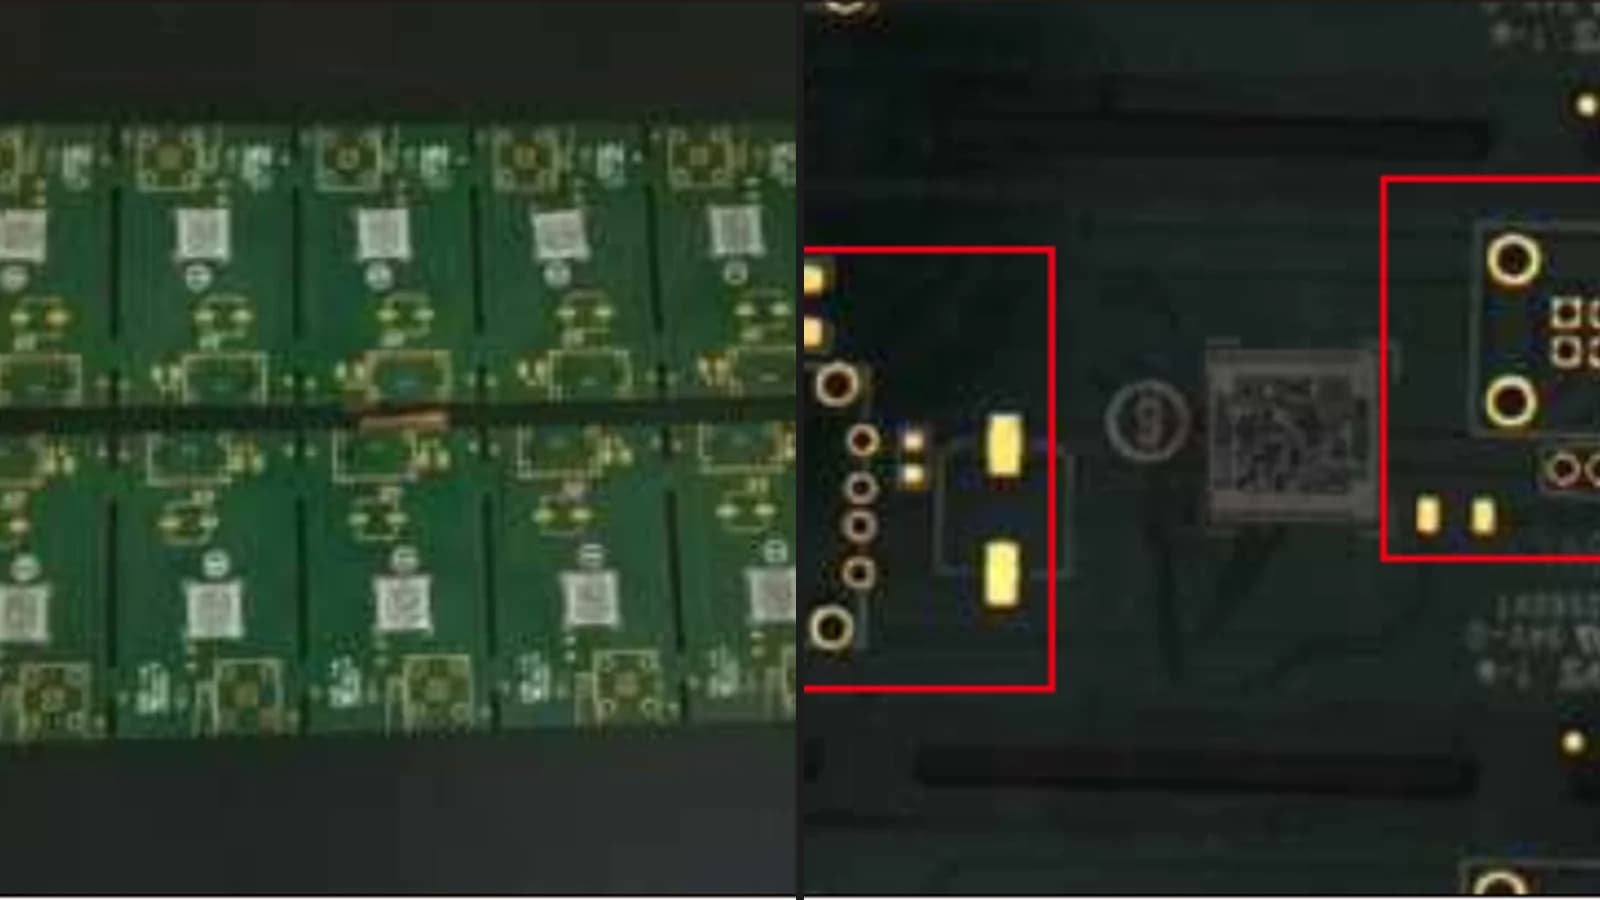
Catalog photograph of a populated circuit board beside the ring-lit result
Left is the populated board. Right is the ring-lit result from a LuxMV application sheet. The red marks are on the sheet.
Selection references

Visual references for selection

These photographs show the shop or the catalog comparison. Send the part to match a series.

AOI multi-angle ring light for PCB solder inspection
Reference 01Multi-angle AOI ring light for solder fillet reflection & bridge contrast control.Send the part or the images with this condition.

Selection considerations

Open the matching series, then send the part or the images.

Which lighting geometry reveals solder joint defects most effectively?

**Multi-tier RGB ring lighting is the definitive standard for SMT AOI defect contrast.** Steep red angle illuminates flat solder, medium green reveals standard fillets, and low-angle blue catches bridging and solder balls.

Technical considerations
  • Coaxial lighting effectively isolates planar laser marks, 2D data matrix codes, and gold finger surfaces.
  • Low-angle ring or bar lighting highlights 3D component edges, tombstoning, and pin height coplanarity.

What environmental and optical parameters determine PCB lighting selection?

**Board material properties and component geometries dictate the required illumination approach.** Target defect (insufficient solder, bridging, polarity reversal), solder mask color, component heights, and pitch are the primary variables.

Technical considerations
  • Camera optical field of view, working distance, telecentric lens specifications, exposure trigger speed, and cycle time must also be considered.

How do component shadows and flux residue affect PCB inspection?

**Flux residue glare and tall component shadows are the leading causes of false rejects in AOI.** Always check solder alloy reflectivity and shadow interference from tall electrolytic capacitors or inductors.

Technical considerations
  • Validate multi-channel LED controller strobe synchronization to precisely isolate each color angle in fast sequential image captures.

Questions for the engineering discussion.

Why are multi-tier RGB ring lights used for PCB solder inspection?

Solder fillets have curved 3D geometries. By projecting Red at a high angle, Green at a mid angle, and Blue at a low grazing angle, the camera captures slope information encoded directly as color variation in a single RGB image.

How do you overcome shadows from tall PCB components?

Use large-diameter coaxial lighting or high-angle diffuse ring lights. These configurations provide nearly perpendicular illumination, penetrating tight spaces between tall capacitors and connectors without casting harsh directional shadows.

What information helps with PCB lighting selection?

Provide good and bad board samples, high-res images, target defects, PCB solder mask color, maximum component height, camera resolution, working distance, and cycle time constraints.

Which illumination geometries correlate to specific PCB solder defects?

Optical configurations for common SMT and through-hole solder joint quality inspections:

PCB solder inspection optical selection matrix
Defect / Inspection FeatureRecommended Illumination GeometryOptical Behavior
Solder Bridging, Solder Balls & ShortsMulti-tier RGB Angle Ring Light (AOI Standard)Different colored LEDs (Red/Green/Blue) at steep, medium, and low angles reflect distinct colors based on solder slope/curvature.
Insufficient Solder, Cold Joints & VoidingLow-Angle Diffuse Ring Light (15° - 30°)Highlights solder fillet climb angle and perimeter boundary while avoiding direct specular reflection back to camera.
SMT Component Shift, Polarity & TombstoningCoaxial / On-Axis Diffuse LightingEven perpendicular illumination captures IC package text, polarity notches, and pad coverage without component shadow.
Gold Finger Scratches & Pad OxidationPolarized Coaxial or Multi-angle Bar ArrayCross-polarization cuts metallic surface glare, exposing sub-surface oxidation and micro-scratches.