LuxMV
See What Matters.
Discuss a project
Application Guide

Semiconductor Inspection Lighting

To achieve sub-micron defect contrast in semiconductor inspection, match illumination wavelength to silicon material physics. Short-wavelength UV (365nm) scatters to expose surface micro-scratches, while SWIR (1050-1550nm) penetrates opaque silicon to reveal internal wafer cracks and hidden solder bumps. Combining specialized spectral bands with coaxial geometries ensures reliable automated defect detection.

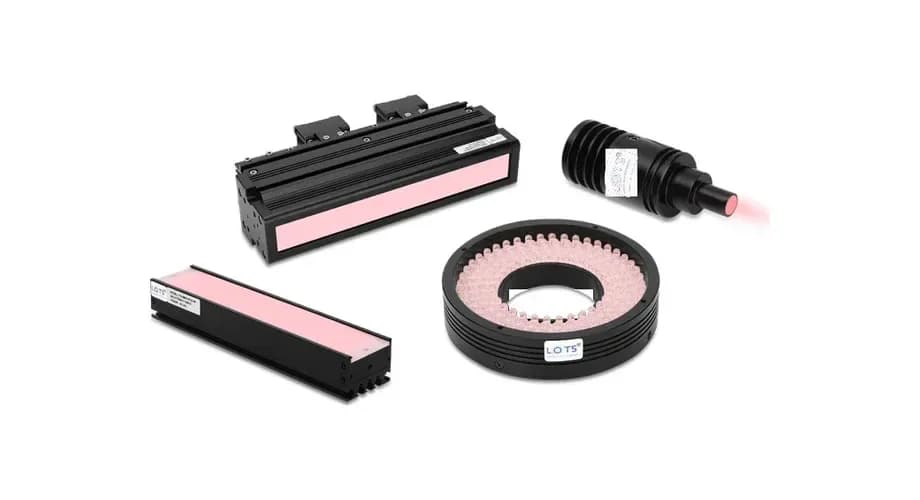
Semiconductor wafer SWIR inspection staging
Short-wave infrared (SWIR) and optical setup for silicon wafer & semiconductor inspection.

Selection considerations

Open the matching series, then send the part or the images.

How does surface topography determine semiconductor lighting geometry?

**Specular reflection control dictates the choice between coaxial, diffuse, and low-angle geometries.** Flat reflective marks, fiducials, or package surfaces: Coaxial or on-axis illumination controls specular reflections from planar targets.

Technical considerations
  • Glossy, curved, or mixed-height package surfaces: Diffuse dome or multi-angle illumination eliminates hot spots and unstable glare.
  • Shallow scratches, chips, edges, or directional texture: Low-angle bar or directional grazing light highlights surface geometry changes.
  • Moving strips, films, or repeated high-speed features: Line-scan lighting with synchronized controller timing ensures pulse exposure uniformity.

Which spectral wavelengths penetrate silicon wafers and carrier tapes?

**Material physics strictly dictate the required illumination wavelength.** Short-wavelength Blue/UV (365nm - 450nm) scatters easily off micro-scratches and shallow surface defects.

Technical considerations
  • Near-Infrared / SWIR (1050nm - 1550nm) penetrates silicon wafers, inspects hidden solder bumps, and sees through carrier tapes.
  • Always verify camera sensor quantum efficiency (QE), lens transmission coating, and filter matching across non-visible spectral bands.

What optical and mechanical parameters constrain semiconductor inspection?

**Physical samples and camera sensor response curves are mandatory prerequisites for lighting specification.** Target part, feature, defect examples, and representative good/bad images or physical samples must be evaluated.

Technical considerations
  • Material stack, finish, coatings, substrate, reflectivity, and any known spectral constraints.
  • Camera model, sensor response, lens, filter, field of view (FOV), working distance (WD), and resolution.
  • Exposure, trigger, motion, line speed, heat limits, cleanliness class, enclosure, and mounting constraints.

How do material variations impact automated optical inspection reliability?

**Optical models that succeed on static samples often fail under dynamic height variation.** Lighting geometry that works on a planar sample may fail on height variation or changing surface finish.

Technical considerations
  • UV, IR, and SWIR setups need compatible cameras, optics, filters, and thermal/safety review.
  • High-speed illumination needs to be checked for exposure, thermal conditions, timing, and uniformity across the field.
  • Production comparison should include representative material and process variation across real wafer lots.

Questions for the engineering discussion.

What lighting should be tested first for semiconductor inspection?

There is no single first choice for every semiconductor task. Start from the inspection objective and surface geometry: coaxial light is often compared for flat reflective features, diffuse lighting for glare control, low-angle lighting for directional surface change, and spectral lighting when the material response requires it.

When should SWIR or IR lighting be considered?

Consider IR or SWIR only when the target material or hidden structure may respond differently outside visible wavelengths and the complete imaging path supports that range. Camera sensitivity, lens and filter transmission, windows, illumination power, safety, and sample images all need confirmation.

What should be included in a semiconductor lighting sample test?

Provide representative good and defect samples or images, material stack or finish when available, target feature, camera and lens, field of view, working distance, line speed or exposure, desired wavelength range, and mounting or cleanliness constraints.

Which lighting spectrums correlate to specific semiconductor defects?

Matching the semiconductor inspection target to the correct optical wavelength and illumination geometry accelerates visual contrast:

Semiconductor defect optical selection matrix
Defect / Inspection TaskRecommended Optical ApproachPhysical Mechanism
Wafer Internal Micro-cracks & Solder BumpsSWIR / NIR Transmission (1050nm - 1550nm)Silicon is opaque to visible light but becomes semi-transparent in SWIR; highlights sub-surface voids and bonding defects.
Wafer Surface Micro-scratches & ParticlesShort-wavelength UV / Blue (365nm - 450nm)Shorter optical wavelengths generate high-angle scattering on shallow topological scratches on mirror-polished wafers.
Mirrored Leadframe & Die Mark OCRCoaxial On-Axis IlluminationEven 90-degree illumination eliminates shadow and isolates laser marks against highly reflective planar leadframes.
Wire Bonding & Solder Ball CoplanarityLow-Angle Darkfield or Diffuse DomeHighlights 3D metallic wire arcs and ball heights while suppressing glare from surrounding shiny substrates.