LuxMV
See What Matters.
Discuss a project
Inspection Guide

Lighting for Reflective Metal Scratch Inspection

On flat polished metal, coaxial light makes the surface bright and a scratch dark, while low-angle darkfield light makes the surface dark and a scratch bright unless aligned with the beam. Compare LXV-3COH, LXV-FPR, and LXV-3DM on the actual part to verify glare suppression and defect contrast.

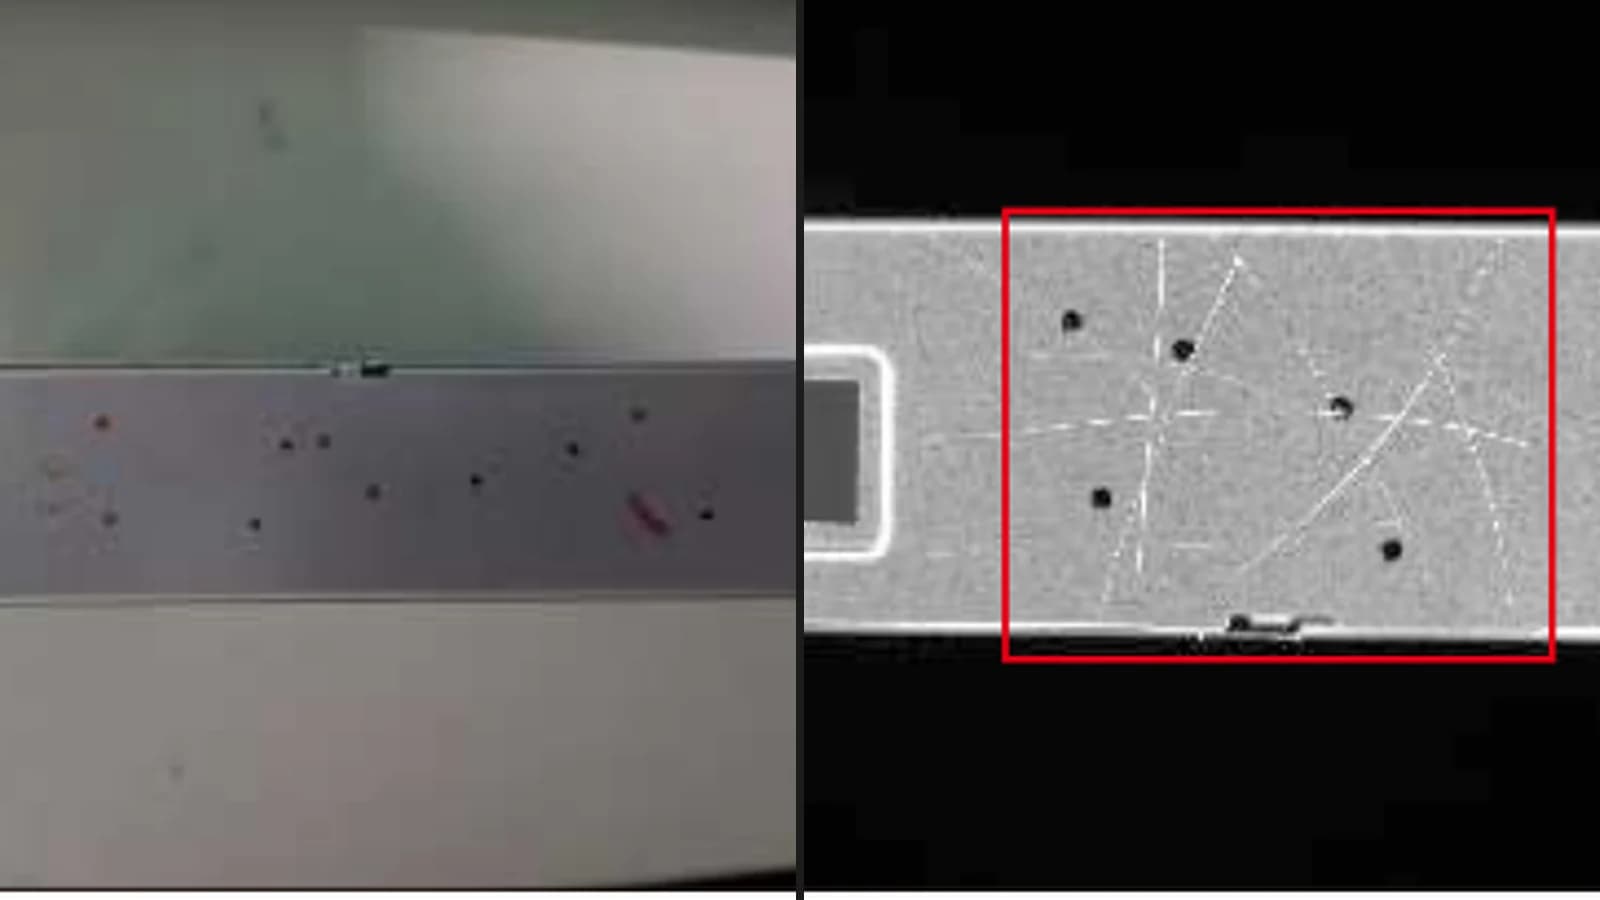
Catalog photograph of a metal surface beside the bar-lit result with scratches visible
Left is the metal surface. Right is the bar-lit result, with the scratch visible.
Selection references

Visual references for selection

These photographs show the shop or the catalog comparison. Send the part to match a series.

Reflective automotive strip defect inspection sample image under controlled lighting
Reference 01Reflective strip evidence shows why glare control and incident angle matter.Send the part or the images with this condition.
Metal screw hole button ring thread and magnetic core inspection evidence image
Reference 02Metal geometry variation should be compared before choosing low-angle, coaxial, or diffuse light.Send the part or the images with this condition.

Selection considerations

Open the matching series, then send the part or the images.

How does low-angle dark-field lighting detect metal surface scratches?

**Low-angle darkfield creates high-contrast shadows across shallow directional defects.** Compare low-angle darkfield bar or ring lighting for directional scratches, coaxial lighting for flat reflective surfaces, and diffuse or polarized setups for curved or glossy parts.

Which optical conditions dictate defect contrast on reflective metals?

**Incident light angle relative to surface topography dictates specular versus scattered reflection.** Record lens and light working distances, field of view, light orientation and mounting clearance for every comparison.

Technical considerations
  • Compare available wavelengths with the actual coating, oil state and sensor sensitivity; do not assume one wavelength removes every reflection.
  • Rotate the part or light to check whether scratches disappear at particular orientations.
  • Record exposure, gain, pulse width, duty cycle and line speed, then verify controller and light limits against their model-specific documentation.

How do surface curvature and finish dictate lighting geometry?

**Surface shape explicitly determines the required illumination angle to avoid localized glare spots.** Shallow scratch, dent, or directional tool mark: Low-angle bar or low-angle ring light creates dark-field shadow contrast across the defect.

Technical considerations
  • Flat mirror-like metal, polished wafer, or planar mark: Coaxial or narrow-angle coaxial light returns uniform on-axis reflection to the camera while isolating edge changes.
  • Curved metal, cylindrical part, or turned component: Dome, diffuse, or polarization light suppresses hot-spot glare and specular reflections on complex geometry.
  • Moving metal strip, continuous foil, or web inspection: Line-scan light with strobe controller maintains exposure uniformity and intensity at high transport speeds.

What are the critical validation steps for metal scratch inspection?

**Physical benchmark testing across part variances is mandatory for reliable deployment.** Compare several low-angle darkfield positions against coaxial illumination on the same samples, keeping camera settings fixed for each comparison.

Technical considerations
  • Retest clean, oily and coated surfaces to identify where a promising lighting setup stops working.
  • Check motion blur and thermal stability at the actual exposure, speed and permitted controller duty cycle.
  • Record pass/fail defect images across multiple part lots to validate contrast stability.

Which application parameters limit lighting setup feasibility?

**Physical mechanical clearance and camera sensor specifications constrain available lighting choices.** Part material composition, surface roughness (Ra), plating, coating, and oil state define optical boundaries.

Technical considerations
  • Defect specification: minimum width/depth to detect, defect orientation, and acceptable contrast ratio.
  • Camera sensor size, lens mount, field of view (FOV), working distance (WD), and mechanical envelope.
  • Grazing light angle aligned with scratch direction causing the defect to disappear.

Questions for the engineering discussion.

Is low-angle lighting always best for reflective metal scratches?

It is a common first test for shallow scratches, but surface finish, curvature, defect orientation, oil films, and line speed may require coaxial, dome, polarization, or strobe illumination.

What information helps with reflective metal lighting selection?

Send part finish, target defect width and depth, camera lens, field of view, working distance, line speed, trigger mode, and representative sample images.

How do I test whether dark-field or coaxial light is better for my specific metal part?

Discuss representative scratched parts, the test scope and sample shipping arrangements with LuxMV. Compare darkfield and coaxial setups using the actual part, and request available drawings for candidate models.

Can LuxMV provide loan units for on-site machine testing?

Ask LuxMV whether evaluation lights or controllers are available for your project. Confirm the selected models, loan terms and test arrangements before planning on-site evaluation.
How do different lighting configurations compare for metal surface inspection?

Reflective metal scratch inspection should be selected from the surface behavior and defect direction, not from a single universal light type. Compare geometry, wavelength, polarization, motion, and sample variation before fixing the final model.

Lighting methods for reflective metal scratch inspection
Lighting methodBest initial fitSelection risk to test
Low-angle bar or ring lightShallow scratches, dents, burrs, and directional tool marksThe defect can disappear if the light is aligned with the scratch direction; compare several incident angles.
Coaxial lightFlat reflective surfaces, planar marks, printed features, and mirror-like metalCurved or uneven surfaces can create unstable glare and require diffuse or polarized comparison.
Dome or diffuse lightCurved, glossy, cylindrical, or uneven metal surfacesDiffuse light can suppress glare but may also reduce contrast for very shallow directional scratches.
Polarized lightingSpecular reflection control on glossy surfaces, films, and coated metalPolarizer angle, lens filter, exposure, and wavelength must be checked together.
Line-scan or strobed lightMoving strip, foil, web, and high-speed metal inspectionLine speed, exposure, pulse width, heat, and controller timing define practical limits.
Catalog models for the three geometries. Angles and working distances are not published as universal values.
GeometryModelWhat the catalog statesWhat this page does not show
Low-angleLXV-FPR24 V low-angle series. Catalog lists eleven sizes from 50 to 230 mm and reduced reflected flare.A scratch parallel to the beam can disappear. The public bar-light photo is not an LXV-FPR record.
CoaxialLXV-3COHCatalog applications include scratches on metal or plastic and short-exposure moving targets.A sloped or curved face sends the on-axis beam away. No paired coaxial photo of the bar-lit sample is published.
DomeLXV-3DMHemispherical diffuse structure for reflective and uneven surfaces.Diffuse light can lower contrast for a shallow directional scratch.