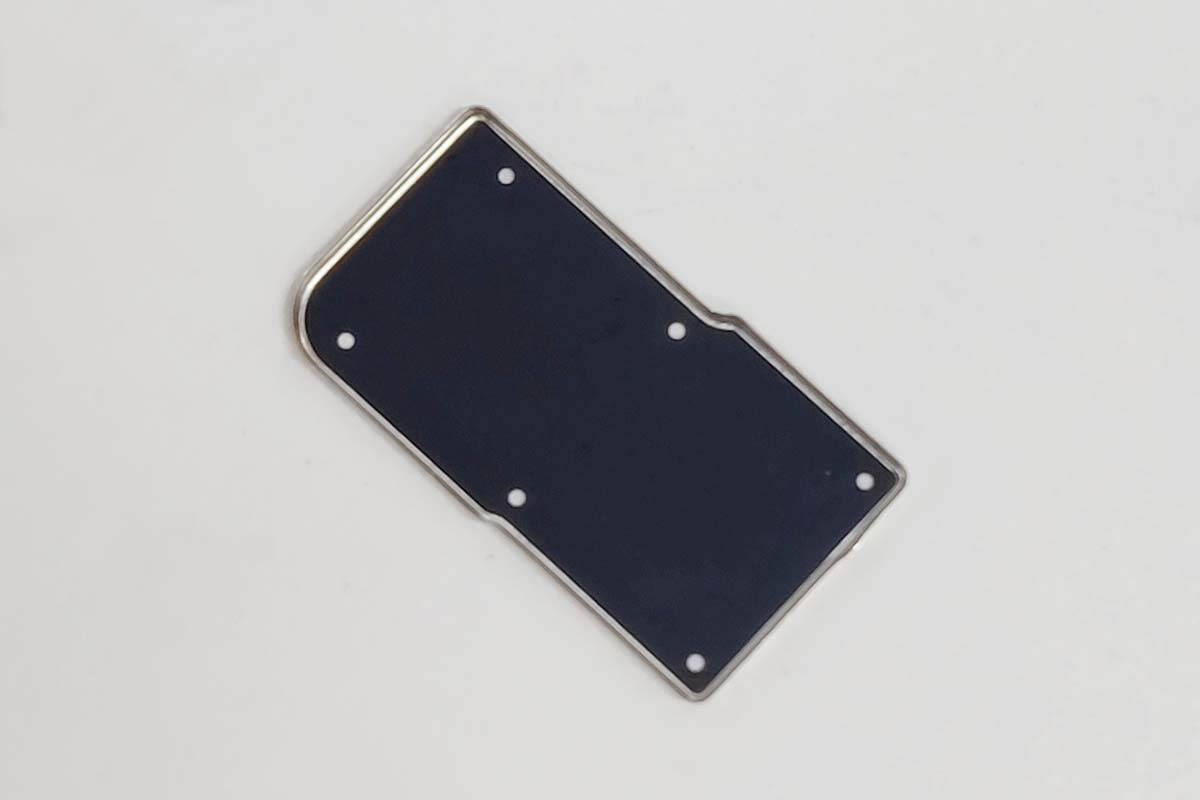
What inspection variables should be evaluated?
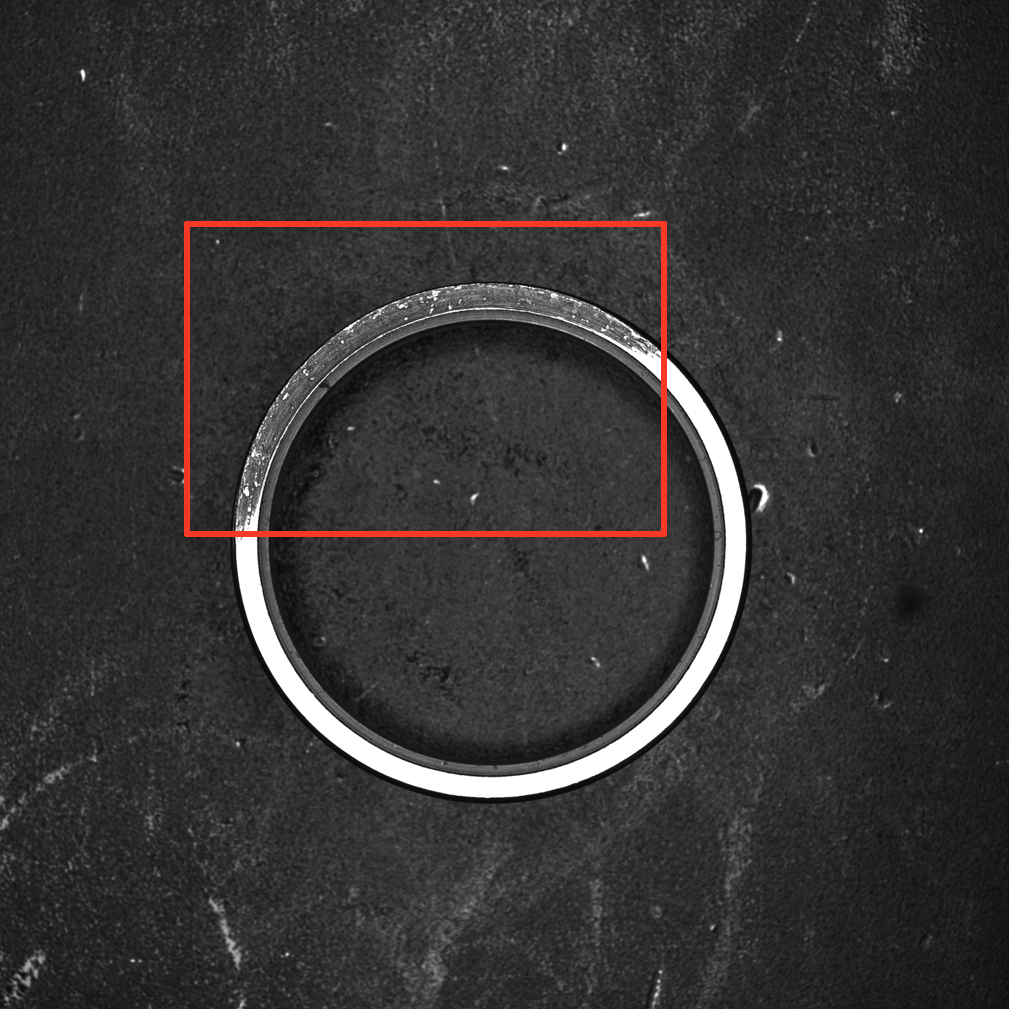
Oil films, machining texture and chamfers can mask hardware defects. Include these normal production variations in validation samples.
What lighting geometry fits this inspection task?
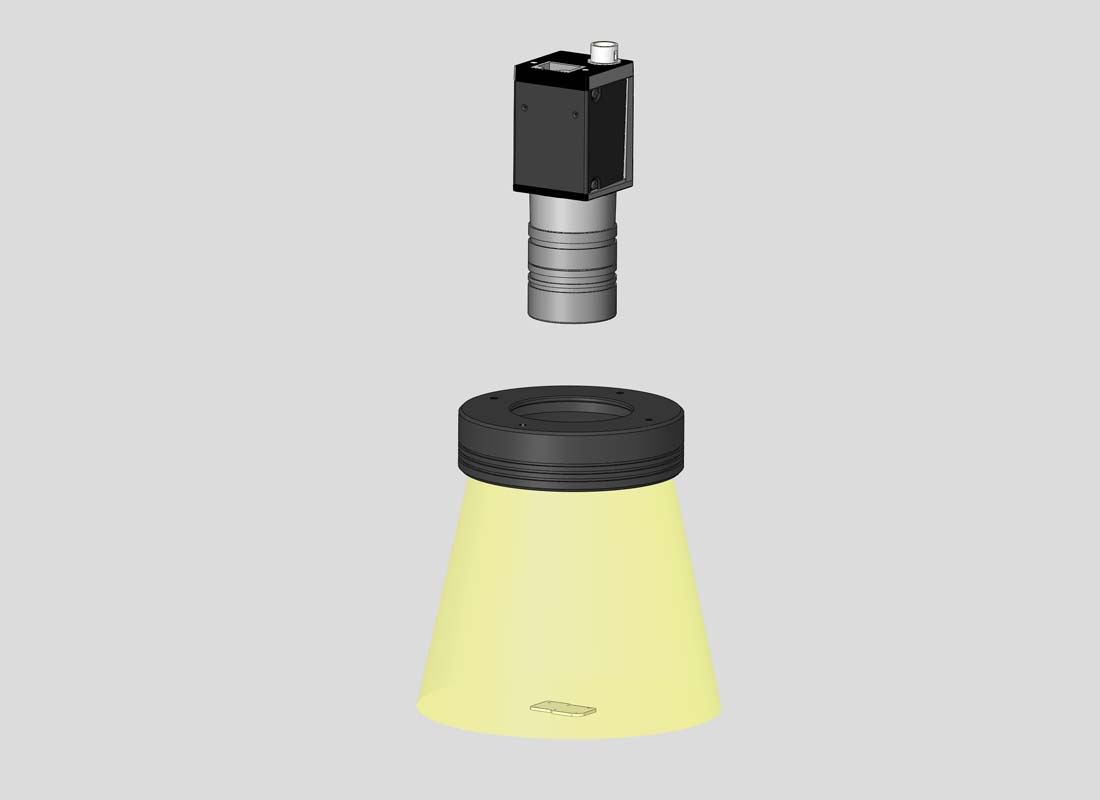
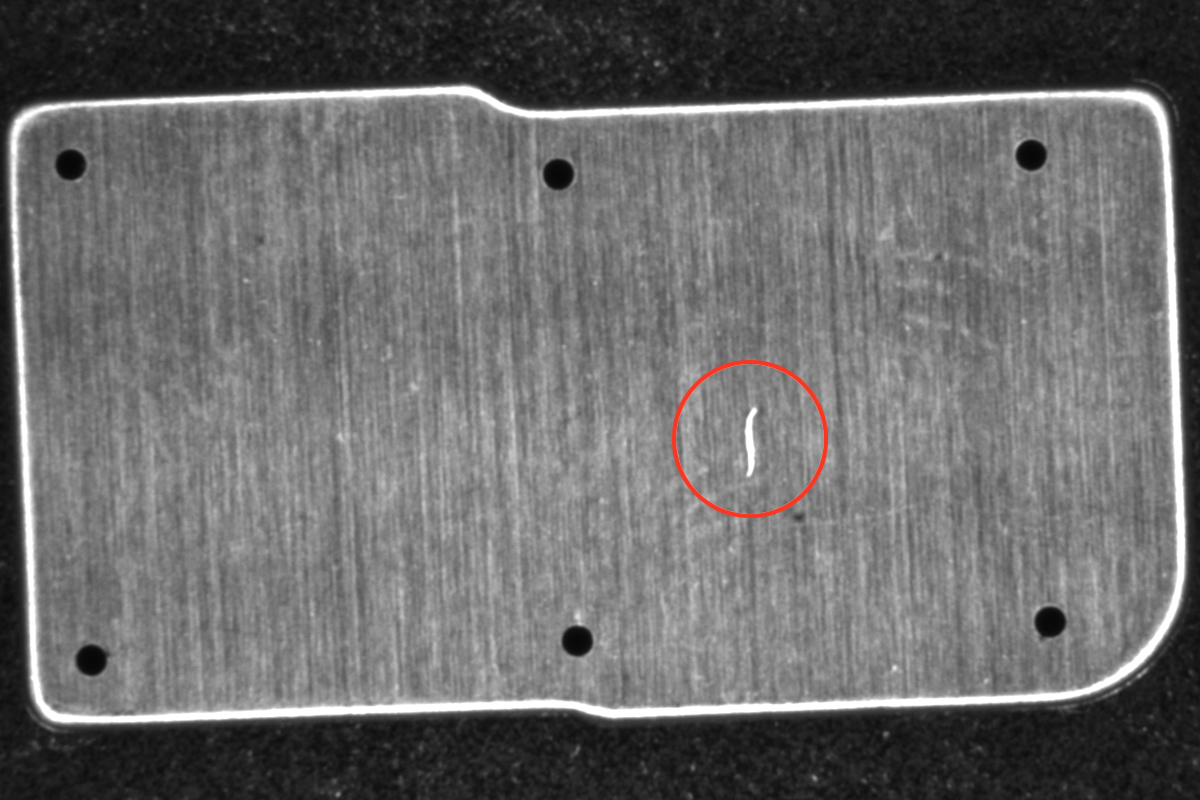
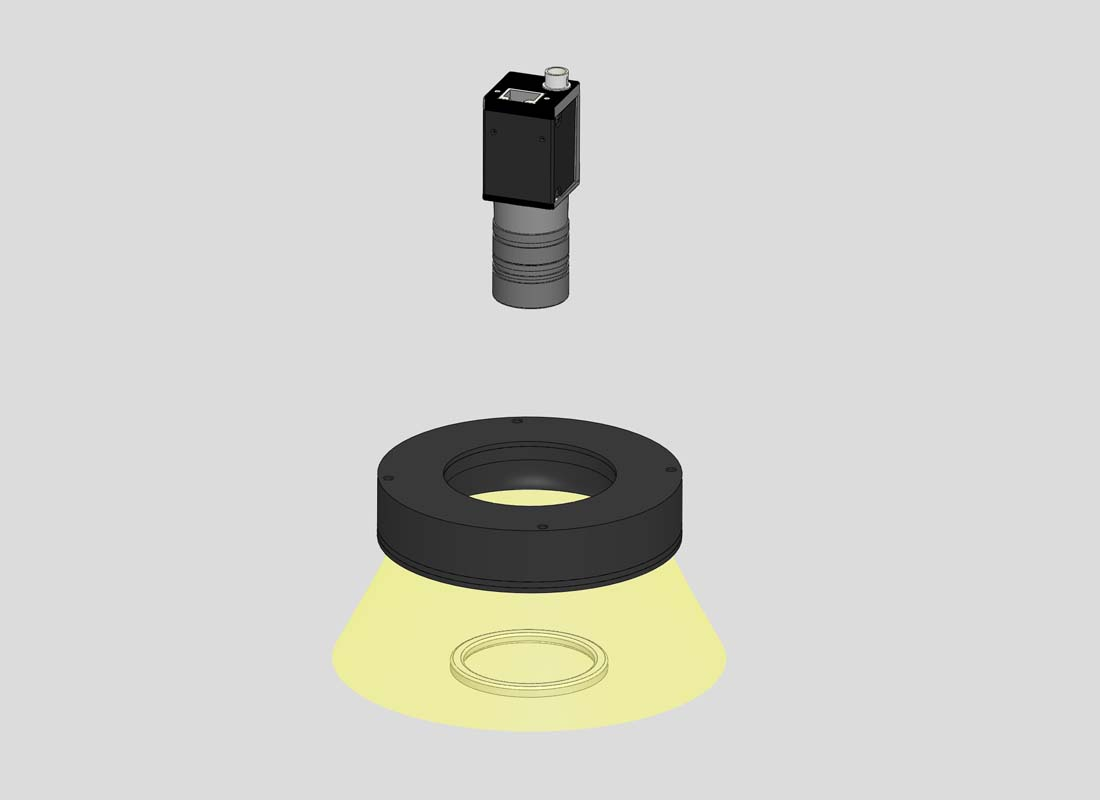
Oblique or low-angle lighting can darken a smooth background while allowing scattered light to reach the camera. Scratch visibility depends on direction, depth and illumination angle. Separate images from several directions may be needed.
Hold the part fixed and vary the light direction. Compare normal texture with actual defects rather than judging brightness alone. Check shadows, curved-surface highlights and motion blur. Repeat the test at production speed and across the permitted position variation before choosing a layout.
Related product family?
LXV-4BR
Lighting for inspecting shapes, surfaces and small details.
Before choosing a configuration?
For selection, specify the field of view, smallest target feature, height variation, cycle time and installation space. Use the specific product page and drawing to verify electrical ratings, dimensions and compatibility.
Choosing the right contrast for metal parts?
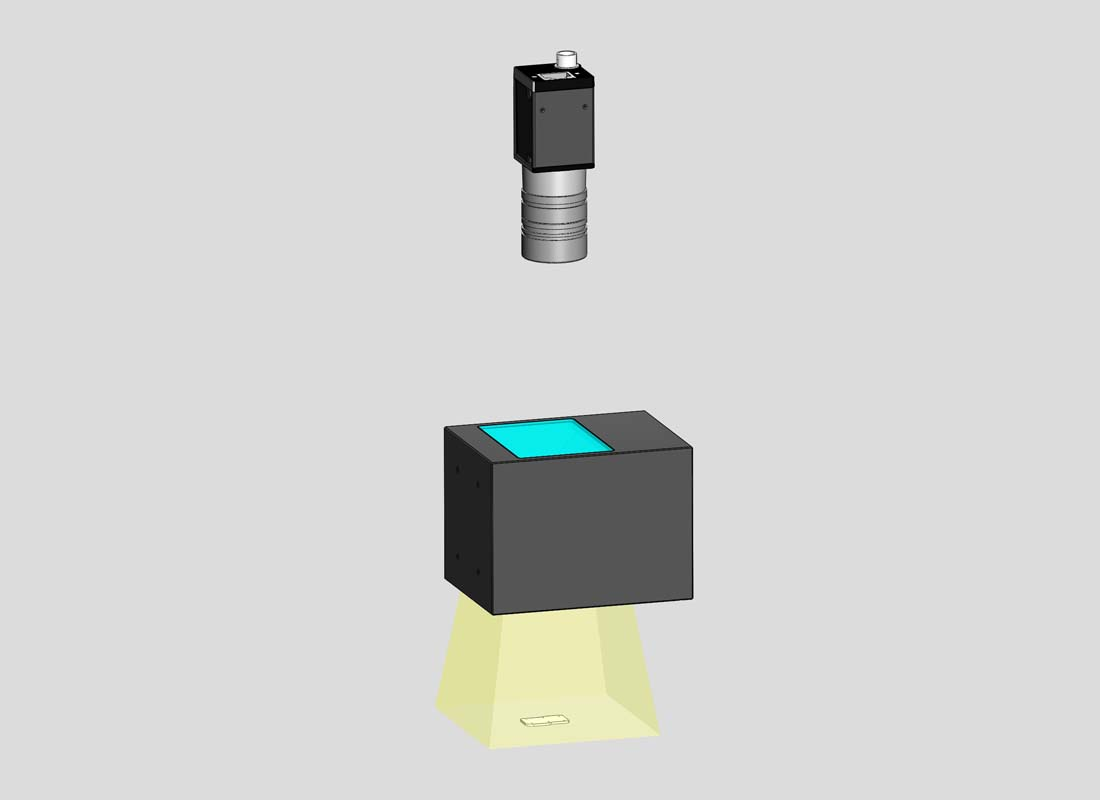
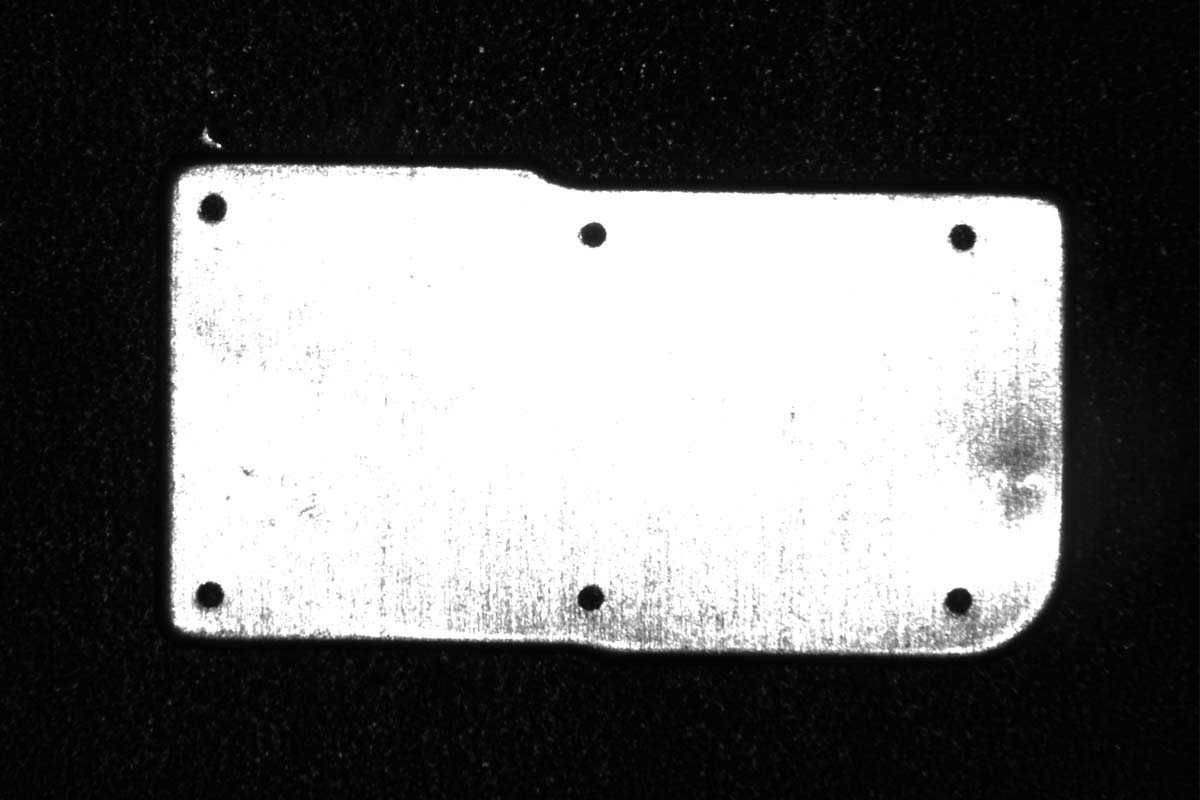
Separate outline measurement from surface-defect inspection. A backlit edge and a reflected-light scratch usually need different geometries. Use the actual finish, including brushed, polished or coated surfaces, in the lighting trial.
Inspect clean parts and known defects at several orientations. Confirm that normal tool marks remain distinguishable from reject features. Check the visibility of holes, steps and recesses that may be shadowed by the fixture.
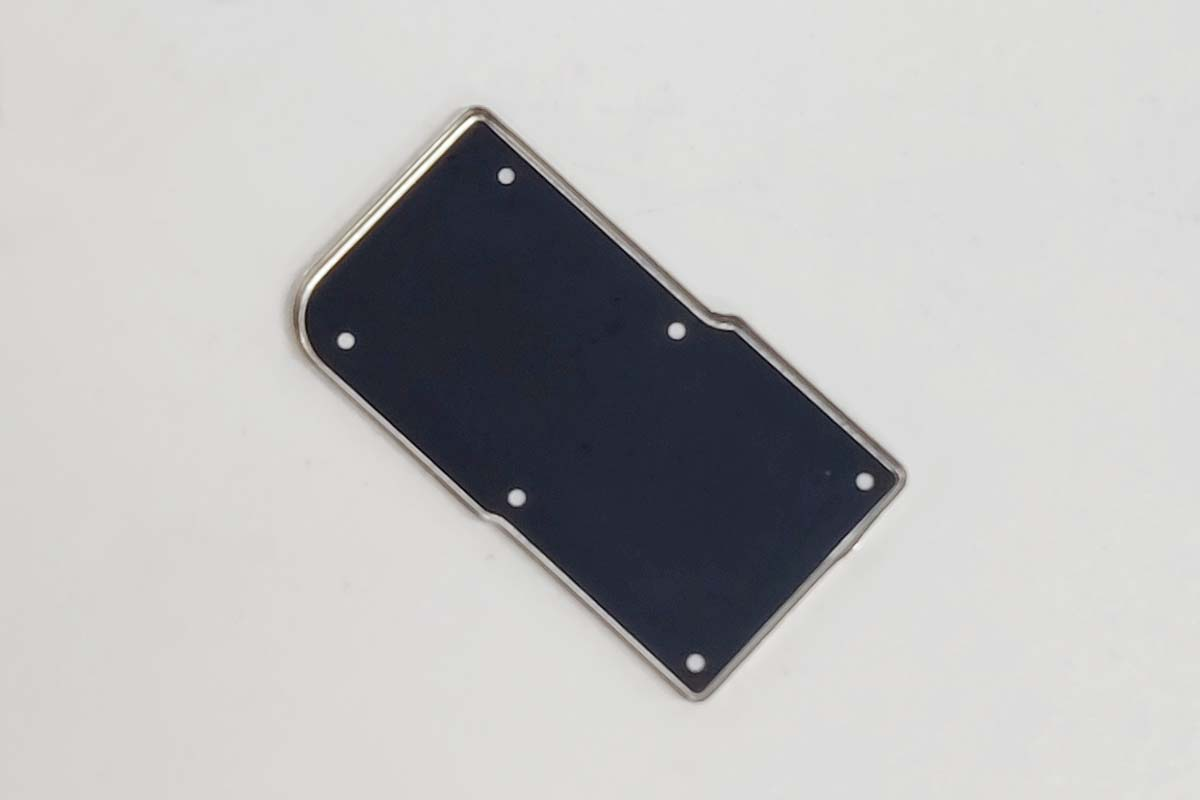
What do the optical setup and sample images show?